CNC production solution for the flexible manufacturing of tapered boards, valley and hip boards, roof crickets and insulation wedges.
The FW5000HR Series was developed for companies that want to produce tapered insulation and roof insulation components from stone wool, PIR, PU and PUR flexibly in their own production.
Tapered boards, valley and hip boards, roof crickets, insulation wedges and custom contours can be produced directly from board or block material.
The special feature of the FW5000HR Series is the combination of CNC contour cutting with a continuously running Fastwire and a conveyor belt integrated into the machine table.
This means one machine performs two production tasks: continuous production of tapered boards from board material and flexible CNC processing of boards and blocks for custom roof insulation components.
For roof applications using EPS, XPS or Neopor, we recommend our RoofCut Series .
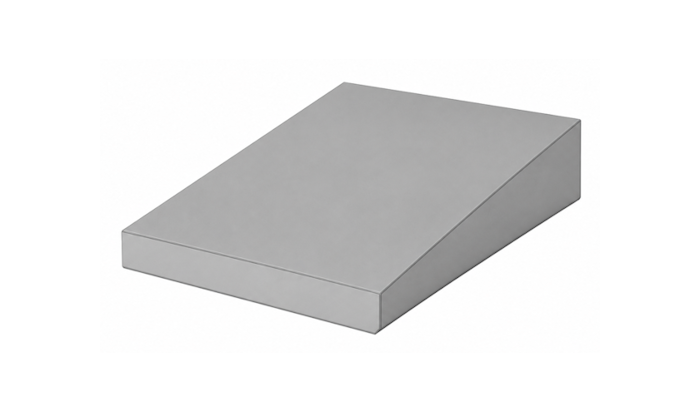
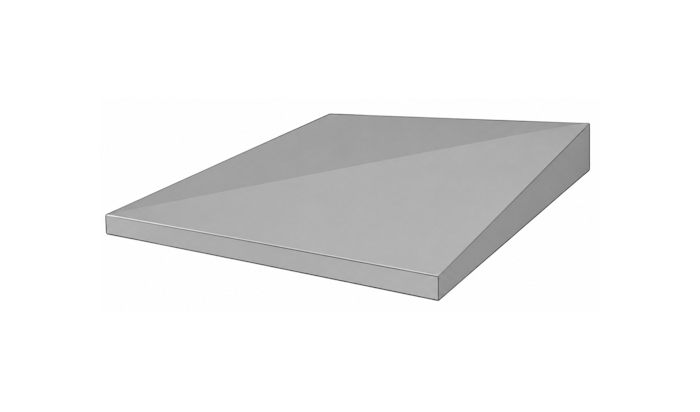
Tapered boards made from stone wool, PIR, PU and PUR for controlled drainage of flat roofs.
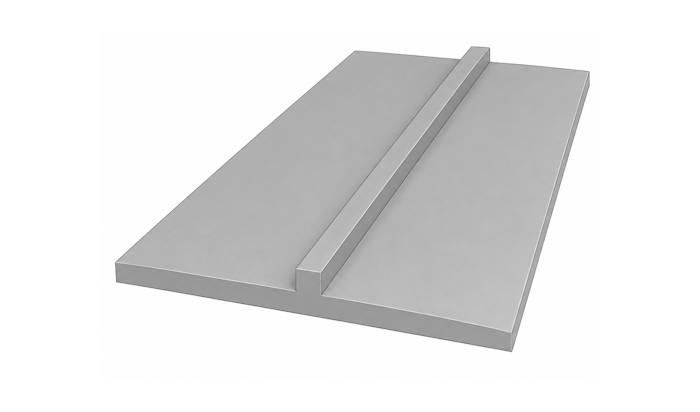
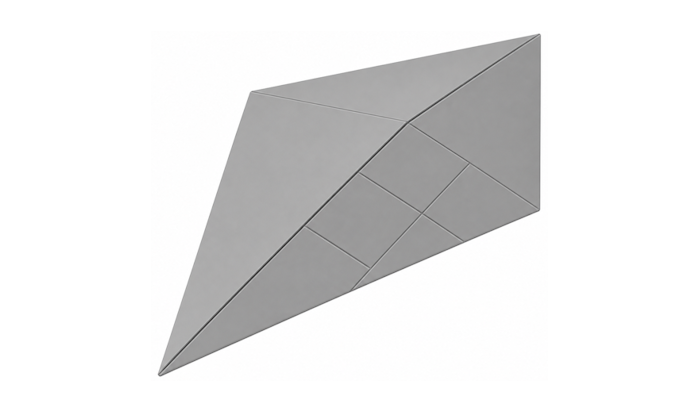
Valley and hip boards for drainage lines, slope transitions and complex roof geometries.
The FW5000HR Series processes stone wool, PIR, PU and PUR. Typical roof insulation components are then produced from 1 × 1 m starting formats.
Stone wool is processed as board material. For roof insulation production, 1 × 1 m boards are generally used, and these can already be ordered in this format.
If longer board formats are used, they can be cut to the required 1 × 1 m starting format on the FW5000HR before the actual processing.
The boards are then processed into tapered boards, valley and hip boards, roof crickets or custom cuts.
PIR, PU and PUR are mainly processed as block material. Common standard blocks are approximately 2,000 or 2,500 mm long.
For roof insulation production, the blocks are first cut into 1 × 1 m starting formats – either directly on the FW5000HR or separately using an additional cut-to-length machine.
The prepared starting formats are then processed into tapered boards, valley and hip boards, roof crickets, insulation wedges or custom cuts.
For roof applications using EPS or Neopor blocks, we recommend our RoofCut Series .
Depending on the starting material and the required roof insulation component, the FW5000HR Series can be used in different ways.
In board operation, individual boards are fed via the front roller conveyor onto the conveyor belt integrated into the machine table.
The conveyor belt transports the boards continuously through the inclined cutting wire. The starting boards are cut into two tapered boards.
The finished boards are then discharged via the rear roller conveyor and can be removed directly or processed further.
In block operation, the block is fed via the front roller conveyor onto the conveyor belt integrated into the machine table and transported into the machine.
A light barrier detects the leading edge of the material and automatically determines the defined material zero point for the subsequent cutting process.
During cutting, the CNC machine table moves the block through the cutting wire in a controlled manner. The two Y axes can move independently.
This makes it possible to produce different slopes, valley and hip boards, roof crickets and other roof insulation components directly from the block.
After the cutting process, the material can be transported via the integrated conveyor belt either back to the starting point or to the opposite side of the machine, where it can be removed or processed further.
In addition to typical roof insulation components, the FW5000HR Series can also cut custom contours from boards or blocks under CNC control using one cutting wire.
This also makes it possible to produce more complex roof insulation components precisely and reproducibly.
Larger PIR, PU or PUR blocks can be cut to the required starting format directly on the FW5000HR before the actual roof insulation production.
For example, standard blocks measuring 2,000 or 2,500 mm in length can be cut into the 1 × 1 m starting formats required for further roof insulation production.
Alternatively, blocks can be cut to length separately using an additional cut-to-length machine. The prepared starting formats are then processed further on the FW5000HR.
The main difference between the FW5030HR and FW5130HR is the available working height. The decisive factors are the board and block heights to be processed and the available building height.
| FW5030HR | FW5130HR | |
|---|---|---|
| X-axis travel | 3,100 mm | 3,100 mm |
| Y-axis travel | 650 mm | 1,400 mm |
| Working width | 1,450 mm | 1,450 mm |
| Max. material height | 600 mm | 1,400 mm |
| Max. material format L × W | 1,450 × 3,000 mm | 1,450 × 3,000 mm |
| Machine dimensions L × W | 7,200 × 2,300 mm | 7,200 × 2,300 mm |
| Machine height | 2,500 mm | 3,500 mm |
| Required building height | min. 2,500 mm | min. 3,500 mm |
| Footprint incl. roller conveyors L × W | approx. 11,200 × 2,300 mm | approx. 11,200 × 2,300 mm |
The actual cutting speed depends on the material and material density. The specific cutting task also affects production time.
For stone wool, typical cutting speeds are approximately 1.0–1.5 m/min.
PIR, PU and PUR are cut at approximately 1.0–2.0 m/min, depending on material density and material structure.
The usable cutting speed depends on the material and material density.
2 tapered boards, 1 × 1 m: approx. 1 minute.
1 valley board and 1 hip board: approx. 2 minutes.
1 roof cricket: approx. 30 minutes.
These figures are practical values and may vary depending on material, dimensions and cutting task.
The FW5000HR cuts abrasively. The fast-running saw wire separates the material mechanically, not with heat. It saws through the material.
There is a suitable cutting wire for every material. Using the wrong wire can significantly reduce its service life.
The cutting wire consists of several cores wrapped with a saw wire. The design of this winding determines which material the wire is suitable for.
Depending on the material, cutting wires with a diameter of 1.2 to 1.6 mm are used. The endless Fastwire runs at up to 300 km/h.
You do not need to write CNC programs to operate the FW5000HR. The important thing is knowing which roof insulation component you want to produce.
Tapered boards and cutting blocks to length run directly via the supplied Roof Standard machine plugin of the machine software. There you enter the dimensions and parameters directly, and the software automatically calculates the required wire position and cutting sequence.
Valley and hip boards as well as roof crickets are created with the optional Roof Pro machine plugin – likewise parametrically and no more difficult to operate. Custom contours can additionally be prepared using the styroCAM CAM software.
Many of our customers familiarize themselves with the applications independently using our instructions or use an application training session with one of our application technicians – at our facility or optionally at your site.
For most roof applications, you need no CAD or CAM knowledge. Typical roof insulation components are created directly using the Roof machine plugin in the machine software. CAM software is also available for custom CNC contours.
For the production of typical roof insulation components, the required dimensions and parameters are entered directly in the machine software.
The supplied Roof Standard machine plugin is designed for producing tapered boards. Based on the entered data, the software automatically calculates the required wire position and cutting sequence.
For valley boards, hip boards and roof crickets, the machine can optionally be expanded with the Roof Pro machine plugin.
CNC programming or your own geometric calculations are not required for these applications.
If roof insulation components or custom cuts are required that cannot be created using the predefined roof functions, custom contours can be prepared using CAM software.
An existing DXF or DWG drawing is imported into the CAM software. The software prepares the contour for the cutting process and generates the machine program.
We supply the FW5000HR Series with our cloud-based styroCAM software. Use of the software is included for the first year.
However, the machine is not tied to styroCAM. Another suitable CAM software package can also be used to create the machine programs.
The FW5000HR Series can be used both for project-specific customer orders and for the pre-production of regularly required roof insulation components.
Tapered boards, valley and hip boards, roof crickets and custom roof insulation components can be produced directly to customer order.
This allows you to respond directly in your own production to different roof geometries, changed dimensions or components required at short notice.
Smaller quantities and replacement production can also be manufactured flexibly without having to order finished roof insulation components from external suppliers.
Regularly required roof insulation components can be pre-produced and stocked.
Frequently required tapered boards and standard dimensions can therefore be produced before a specific customer order exists.
This creates your own inventory and allows you to respond to new orders faster and more independently of external lead times.
If service is required, support is provided directly by cnc-multitool.
Many issues can first be analyzed together by phone, email or remote support and can often be resolved directly.
The FW5000HR is designed so that important components are easily accessible and can be replaced quickly when required. After consultation with our service team, many tasks can also be carried out by your own employees.
If an on-site repair is required, a service technician can carry out the necessary work directly at your facility.
The objective is always to keep downtime as short as possible and return the machine to production quickly.
The FW5000HR Series is designed as a robust CNC Fastwire roof cutting machine for daily processing of stone wool, PIR, PU and PUR in production.
The machine table is designed as a stable, open steel structure for processing boards and larger material blocks.
A conveyor belt is integrated into the machine table. This allows the material not only to be positioned, but also to be moved through the machine in a controlled manner during the production process.
An integrated light barrier detects the leading edge of the material and provides a defined material zero point for the cutting process. This simplifies repetitive production processes in particular and ensures reproducible material positioning.
The open design keeps the work area easily accessible. Boards and blocks can be placed and aligned easily and, if required, processed directly on the machine table.
The FW5000HR Series has two independently controlled Y axes on the left and right sides of the cutting wire.
This allows the cutting wire to be positioned at different heights on both sides of the machine. In addition to straight cuts, this also enables defined slopes and different height profiles.
This independent axis control forms the technical basis for producing tapered boards, valley and hip boards, roof crickets and other more complex roof insulation components.
For normal straight cuts, both axes can operate together. If different heights are required, YL and YR are positioned independently as needed.
The continuously running cutting wire is tensioned during operation by a pneumatic wire tensioning system.
Consistent wire tension is important so that the cutting wire is guided cleanly and achieves precise and reproducible results even during longer cuts.
The cutting wire is also monitored continuously. If a wire break is detected, the machine shuts down automatically and stops.
After the cutting wire has been replaced, the cutting process can be continued from the last position.
Fastwire cutting generates dust and fibers depending on the material. The cutting arms of the FW5000HR are therefore enclosed and prepared for connecting a suitable dust extraction system.
For this purpose, two 100 mm extraction ports are available directly on the cutting arms.
Roller conveyors for material feeding and unloading are installed in front of and behind the machine.
Boards and blocks can therefore be moved to the machine at working height and transported out of the working area again after cutting.
Especially for larger or heavier materials, the roller conveyors simplify handling and reduce the amount of manual movement required.
Together with the integrated conveyor belt, this creates a continuous material flow from loading to unloading.
Together with the machine software, control and Roof machine plugin, the computer system forms the operating environment of the FW5000HR Series.
The system is prepared for machine operation and is supplied with a current Windows Pro license, ensuring that the computer, interfaces and software are coordinated with one another.
All cnc-multitool computer systems feature a second SSD as a backup drive.
The operator console is located directly at the FW5000HR and is designed with dust protection for use in the production environment.
Computer, monitor, keyboard, mouse and the operating elements required for machine operation are arranged clearly at a fixed workstation.
This means machine operation, software and production documents are located exactly where they are needed in daily production.
The operator can monitor the machine, set up the material and control the cutting process directly from the workstation at the machine.
The most important technical data of the two machine versions compared directly.
| Feature | FW5030HR | FW5130HR |
|---|---|---|
| CNC axes | 3 | 3 |
| X-axis travel | 3,100 mm | 3,100 mm |
| Y-axis travel | 650 mm | 1,400 mm |
| Working width / cutting width | 1,450 mm | 1,450 mm |
| Max. material height | 600 mm | 1,400 mm |
| Max. material format | 3,000 × 1,400 mm | 3,000 × 1,400 mm |
| Number of cutting wires | 1 | 1 |
| Wire diameter | 1.2 – 1.6 mm | 1.2 – 1.6 mm |
| Wire inclination / skew | up to 10% | up to 10% |
| Cutting wire speed | up to 300 km/h | up to 300 km/h |
| Cutting wire drive | 4 kW | 4 kW |
| Max. cutting speed | up to 4 m/min | up to 4 m/min |
| Max. positioning speed | 6 m/min | 6 m/min |
| Max. conveyor belt speed | 3 m/min | 3 m/min |
| Roller conveyor length | 2,050 mm | 2,050 mm |
| Drive | Rack / chain | Rack / chain |
| Pneumatic wire tensioning | Standard | Standard |
| Wire break monitoring | Standard | Standard |
| Compressed air | 6 bar | 6 bar |
| Power supply | 400 VAC, 50–60 Hz | 400 VAC, 50–60 Hz |
| Power consumption | approx. 5,000 W | approx. 5,000 W |
| Machine dimensions (L × W × H) | 7,200 × 2,300 × 2,500 mm | 7,200 × 2,300 × 3,500 mm |
| Footprint incl. roller conveyors (L × W) | approx. 11,200 × 2,300 mm | approx. 11,200 × 2,300 mm |
| Approx. machine weight | 950 kg | 1,150 kg |
| Technical datasheet | ||
| Price plus VAT | 68.500,00 € | 72.500,00 € |
| Request | Request |
The FW5000HR Series is supplied as a complete production solution. The machine, material handling, control and basic software are already included.
Fastwire cutting generates cutting dust. Stone wool additionally produces fiber-containing dust, which should be captured as close as possible to the cutting area.
A suitable dust extraction system is therefore required for production operation.
We offer a dust extraction solution matched to the FW5000HR that can be switched on and off via the machine software.
Alternatively, a customer-provided dust extraction system can be integrated into the machine.
A suitable safety system is required for machine operation.
Depending on the installation and production environment, it can consist of a safety fence and safety light barriers.
The safety system can be ordered from us or provided by the customer in accordance with the applicable safety regulations.
For heavy or large-format boards, the FW5000HR Series can be equipped with a lifting aid for material loading.
This allows stone wool, PIR, PU or PUR boards, for example, to be picked up and ergonomically positioned on the front roller conveyor or at the machine infeed.
The lifting aid reduces the physical strain on the operator and simplifies regular machine loading.
The Roof Pro machine plugin expands the machine's standard functions to include the production of valley boards, hip boards and roof crickets.
The operator enters the required dimensions and parameters. The software automatically calculates the geometry, required wire position and complete cutting sequence.
There are two options for commissioning the FW5000HR Series.
On request, our technicians can carry out installation and commissioning directly at the customer's site. The machine is assembled, connected, tested and handed over ready for operation.
Alternatively, the FW5000HR Series can also be commissioned by the customer. We provide the relevant documentation and videos and can also provide remote support if required.
In addition, software and application training can be booked at cnc-multitool, at the customer's site or online via TeamViewer.
The FW5000HR Series is designed for processing stone wool, PIR, PU and PUR – stone wool mainly as board material, PIR, PU and PUR mainly as block material.
Yes. The FW5000HR Series can process both boards and blocks: boards run continuously through the cutting wire via the integrated conveyor belt, while in block operation the material is moved on the machine table under CNC control.
The main difference is the available working height: the FW5030HR has a Y-axis travel of 650 mm, the FW5130HR 1,400 mm (working width 1,450 mm each) – the available building height must also be considered.
Yes. In addition to typical tapered boards, valley and hip boards, roof crickets and custom CNC contours can be produced from boards or blocks.
Yes. Standard PIR, PU or PUR blocks can be cut directly on the FW5000HR into the 1 × 1 m starting formats required for roof insulation production – alternatively separately using a suitable cut-to-length machine.
The scope of supply includes the Roof Standard machine plugin for producing tapered boards: dimensions and parameters are entered directly, and the required machine movements are then calculated automatically.
No separate CAM programming is required for typical roof applications; for free and custom contours, suitable CAM software can be used.
The cutting wire is monitored during operation: if a wire break occurs, the machine shuts down automatically, and after replacing the wire the cutting process can be continued from the last position.
Yes. The machine requires 6 bar compressed air for the pneumatic wire tensioning system.
Yes. Fastwire cutting generates cutting dust, so a suitable dust extraction system is required for operation – supplied by cnc-multitool or provided by the customer.
Yes. A suitable safety system is required for operation; the specific design depends on the installation, production environment and applicable safety requirements.
Yes. You can provide us with your own material or bring it to a demonstration in Ilmenau, so we can jointly check the cutting wire, cutting speed and cutting quality for your application.
Would you like to see how stone wool, PIR, PU or PUR can be processed on the FW5000HR?
Visit us in Ilmenau and experience the machine under real production conditions. You are also welcome to bring your own material and test it together with us.
This allows us to determine directly which machine version, cutting wire and equipment make sense for your production.
Request demonstration